

Profiling plantLinia CZS
Zeman




Temel veriler
- Makine adı:
- Profiling plant
- Üretici:
- Linia CZS
- Model:
- Zeman
- Üretim yılı:
- 2010
- Durum:
- yeni gibi (kullanılmış)
- Işlevsellik:
- tamamen fonksiyonel
Fiyat ve Konum
- Konum:
- Mariusza Bojemskiego 9, 42-202 Częstochowa, Polska
Teklif detayları
- İlan Kimliği:
- A21299532
- Son güncelleme tarihi:
- 22.10.2026
Açıklama
ZEMAN CZS LINE SPECIFICATIONS.
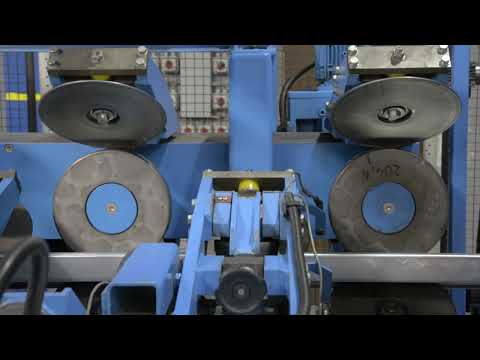
ZEMAN's flagship product, the fully automated "PURLIN" line, is used to produce open, cold-formed sections such as C, Z, and SIGMA, in various widths and shapes, thanks to fully automatic adjustment of the profiling rollers. Coils up to 750 mm wide and 1.25 mm to 3 mm thick sheet metal in grade S-390 and lower can be used as raw material. The machine is designed to produce components up to 15 m long. The width of the specially hardened profiling rollers is infinitely adjustable, using only dedicated software. A fully integrated "flying punching" device creates all types of mounting holes, and the entire process is continuous, meaning the material does not stop for individual operations such as punching holes or cross-cutting. To maintain production efficiency, the line speed is dynamically optimized. The machine decelerates and accelerates automatically without operator intervention.
A coil uncoiler with a maximum working load of 15 tons is mounted on a mobile trolley, enabling precise centering of the material strip before feeding it into the straightener.
The straightener, along with a crescent straightening system, allows for straightening the material, ensuring the required sheet flatness and reducing the crescent on the feed belt.
2. Punching Section
This section contains 5 double, "flying" punching portals, which can be equipped with 20 small (up to 40 mm) or 10 large (up to 100 mm) tools (punches and dies) for punching mounting holes.
A combination of these tools can also be used.
3. Pre-cutting Shear
A "flying" shear used to make preliminary holes for the cutting shear. This process is designed to maintain material continuity, resulting in a more precise profile shape, especially at its beginning and end. This is an adaptive guillotine that adjusts the width of the hole being cut to the width of the sheet metal strip.
4. Guide Carriage/SIGMA Modules
The guide carriage is used to center the sheet metal strip before entering the profiler. It is interchangeable
with the module for producing Sigma-shaped profiles. To produce S+ profiles,
the guide table should be removed and two Sigma modules inserted. These modules position
fully automatically and independently, left and right.
6. Rotary Cut-Off Guillotine.
Bwedpfxjymampj Apaow
The rotary cut-off guillotine with hook knives is used to finally cut the profile from the material strip
using the holes made by the pre-cutting guillotine. This is a "flying" guillotine,
so the sheet metal does not stop during the cutting process. Depending on the profile being produced, a properly oriented cutting cassette should be attached.
7. Receiving Table
The receiving table is used to automatically discharge the completed profiles from the roller conveyor. The elements are then manually arranged into a package. The design allows for easy bundling of the package. The table is designed to accept 15-meter profiles and allows for access by a forklift or overhead crane to collect the package of profiles.
Tedarikçi
En son çevrimiçi : geçen hafta
Kayıtlı seit: 2006
175 çevrimiçi ilan

İstek gönder
Telefon & Faks


 Weilerswist
TEMAREDCar Flat 3518 für PKW bis 1.438 kg - Kippbar


 Beograd
GaspariniSlitter


 Vilalba
DemaqEvo 4.0


 Moldova
Mechanika MaszymLRV


 Almanya
GildemeisterCTX 200E


 Staufenberg
DURMAAD-S 30175


 Düsseldorf
DECKEL MAHODMF 250 Linear

 Fevziçakmak
TFON MACHINE CO.Leveling Machine | TF-L 9016


 Hagen
DMGDMC 1035 V


 Ciriè
STAMSTAM-2000

Machineseeker-güven damgası
Güven damgası nedir?
Machineseeker, Machineseeker güven damgası ile seçili bayileri sertifikalandırmaktadır. Tahsis öncesinde deneyimli Machineseeker personeli tarafından standartlaştırılmış ve kapsamlı bir kontrol gerçekleştirilir.
Ne kontrol ediyoruz?

Ticaret izni veya ticaret sicil özeti kontrolü
Satıcının
posta adresinin kontrolü
Banka bağlantısı doğrulama
Ana numaranın
telefonla
erişilebilirliğinin doğrulanması
Ekonomik bilgi
olumsuz özellikler içermemelidir
Alıcı Şikayetleri
mührün geri çekilmesine yol açabilirBu, bir alıcı olarak sizin için ne anlama geliyor?
Machineseeker güven mührü sayesinde, alıcı olarak kendi kontrolünüz olmadan büyük olasılıkla dürüst ve güvenilir ticaret yapan güvenilir satıcıları tanıyabilirsiniz.
Elbette, satın alma sürecinde yine de anlaşmazlıklar ortaya çıkabilir. Machineseeker, Machineseeker platformunda aktif olan alıcıların veya satıcıların yasal ihlallerinden sorumlu değildir.